Introduction
Tubular Drag Conveyor has the characteristics of good sealing, less dust leakage during conveying, and flexible layout, which is suitable for materials with high requirements for sealed conveying. However, during the actual operation process, the stability of the Tubular Drag Conveyor not only depends on the performance of individual components such as chains, flights (disc scrapers), and drive devices, but is also closely related to factors such as conveying pipe straightness, inlet and outlet port structures, pipe chain tension degree, and material operating status. Especially for equipment with long conveying pipes and very small clearances between flights and pipe walls, local pipe deformation or flight abnormalities may lead to friction, jamming, and vibration, further causing pipe heating, damage to flights and connecting plates, and in severe cases, even causing equipment accidents such as damage to head supports and foundations.
Failure Phenomena
During daily operation, the Tubular Drag Conveyor showed abnormal phenomena such as obvious vibration at the head and tail, obvious local jittering of the chain, loud operation sound, and severe heating in some pipe sections.
During one operation, a serious equipment accident occurred: the head support foundation was damaged, the reducer foundation suffered a certain degree of damage, and multiple flights and connecting plates were damaged.
Failure Causes
The body pipe is relatively long. Due to installation, vibration, and connecting pipe thermal expansion and contraction deformation stress, local bending deformation was caused. To ensure material conveying efficiency, the clearance between the flight and the inner wall of the pipe is very small, so during equipment operation, the flight easily rubs against the inner wall of the deformed pipe, causing severe heating in parts of the pipe.
The connections between the inlet/outlet ports, head/tail, and the main body of the Tubular Drag Conveyor are right-angle connections. The connection transitions are not smooth, and the internal welds at the right-angle connections are not polished smooth. The circled part shows the situation when the flight runs to the right-angle edge. The flight will inevitably be caught and tripped by the right-angle edge, causing the pipe chain to jitter, thereby causing large vibrations at the head and tail.
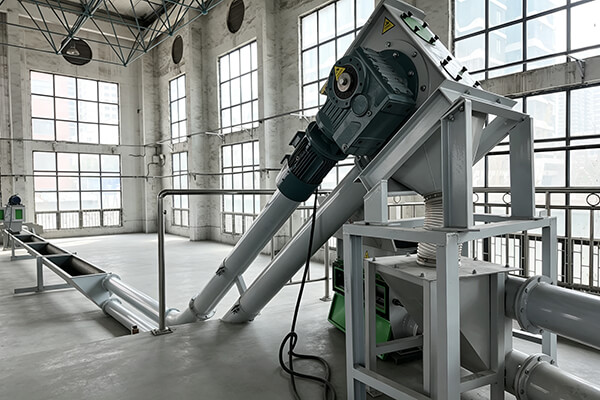
If the pipe chain is too loose, on the one hand, it will cause friction between the flight and the bottom of the body pipe, causing pipe heating; on the other hand, when the flight runs to the connection between the body pipe and the upper inlet port or the head and tail, jamming will occur, causing body vibration.
Deformation of flights and connecting plates. The flight is processed from wear-resistant resin material into a certain shape, with a stainless steel connecting ear integrated and passing through it. The connecting plate is a long strip-shaped 4mm thick stainless steel plate with round holes at both ends. Flights are connected via connecting plates and pins to form a pipe chain. Due to factors such as material resistance, pipe rubbing, and mutual pulling force between flights, flights and connecting plates will undergo bending deformation after long-term operation. When running to the sprockets at both ends, sticking will occur, and in severe cases, it will lock up with the sprockets. At this time, it will cause the pipe chain to be pulled to break and the head support to be pulled out. The situation of flights and connecting plates meshing with sprockets under normal state.
The Tubular Drag Conveyor rotates counterclockwise. Material will be carried along the upper conveying pipe by flights to the tail for a short stay, and then sent along the lower pipe to the discharge outlet. When the load is large, material at the tail will correspondingly increase, producing large resistance to the pipe chain, which will cause damage to flights and pipe chains after long-term operation.
Repair Conditions and Effects
Correcting Deformed Pipes
By making tooling and adding shims at pipe supports, the pipe straightness was adjusted using a thin stretched string as a benchmark line. Since the clearance between the flight and the inner wall of the pipe is only 2.5mm, the distance difference between each section of the body pipe and the benchmark line should be adjusted to within 2.5mm to ensure pipe straightness.
The upper silo and 3 inlet ports of the Tubular Drag Conveyor are rigidly connected through stainless steel pipes. Stress changes generated by the silo due to factors such as temperature and feeding directly act on the Tubular Drag Conveyor through the connecting pipes, thereby causing body pipe deformation. In response to this situation, 200mm was cut from each of the connecting pipes between the 3 inlet ports and the upper silo, and silicone flexible connections were added, thereby eliminating the influence of the silo on the Tubular Drag Conveyor.
Modifying Tubular Drag Conveyor Tripping Places to Arc Transitions
Originally, the connections between the inlet/outlet ports, head, and tail parts and the body pipe of the Tubular Drag Conveyor were right-angle connections. The right-angle edge would block the smooth operation of flights. The right-angle connections were modified to arc connections. After improvement, flights can pass smoothly, avoiding vibrations generated by the right-angle edge blocking flight operation.
Replacing Deformed Flights and Adjusting Pipe Chain Tension
Inspect the pipe chain, replace deformed flights and connecting plates to prevent deformed connecting plates from locking up with sprockets. Adjust the tension of the pipe chain by adjusting the distance of the tail and increasing or decreasing the number of flights. During operation, judge the tension degree of the pipe chain by observing whether there is chain jittering through the observation port and whether there is collision and friction sound between the pipe chain and the body pipe. If the pipe chain is found to be loose, it should be adjusted in time.
Adding Upper and Lower Pipe Communication Pipes
At the tail, the upper and lower conveying pipes were connected together, which reduced the conveying path of materials, reduced the running resistance of the pipe chain, and improved running stability.
Conclusion
Through systematic analysis of failure causes and targeted improvements for the Tubular Drag Conveyor, the equipment running condition has been significantly improved: head and tail vibrations were greatly reduced, chain jittering and abnormal running sounds were basically eliminated, abnormal pipe section heating issues were resolved, severe equipment accidents did not occur again, equipment operational stability and reliability were greatly improved, meeting the production requirements of sealed conveying for polyoxymethylene (POM) powder, while also providing reference practical experience for failure troubleshooting and structural improvement of similar types of conveying equipment.